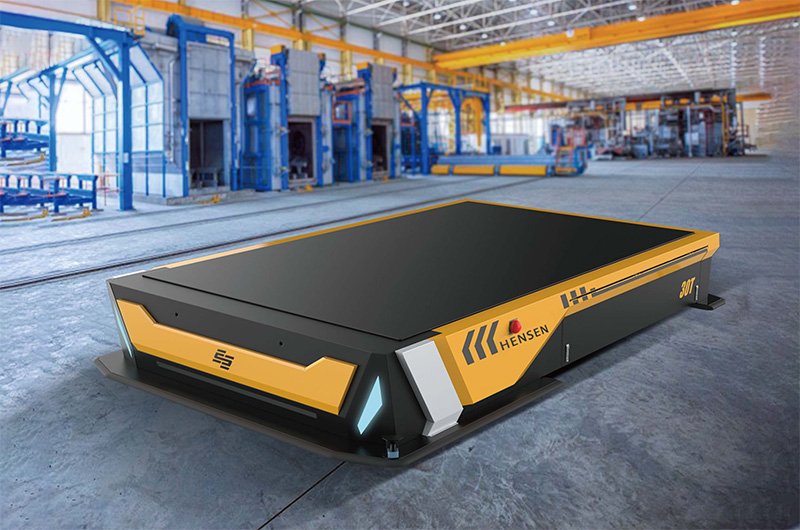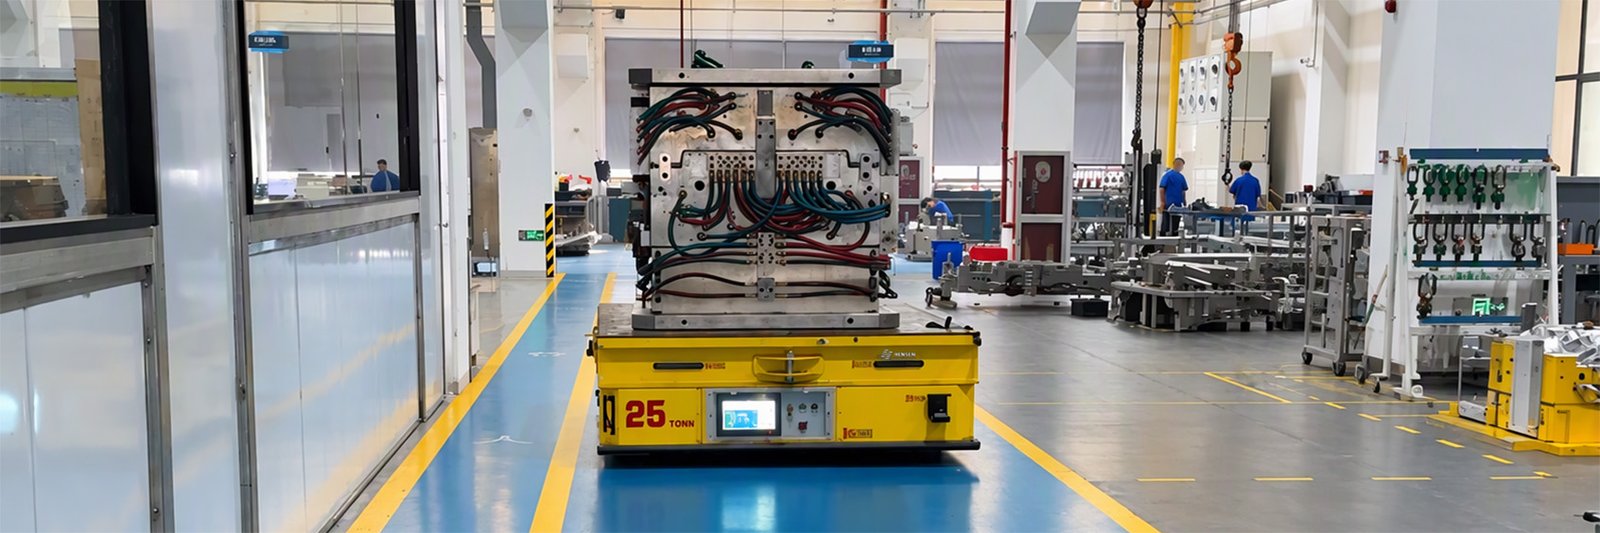
HENSEN designed a custom mold transfer system for a mold manufacturer in Taizhou, China, combining six 25-ton automated guided vehicles (AGVs), automatic charging and centralized fleet dispatching. The project connects precision machining, assembly, and mold trial areas, with an MES interface specified to link transport requests to production process plans.
The engineering challenge was to move heavy molds between many workstations while accommodating changing destinations, shared aisles, and return trips for rework. A compact vehicle platform and process-based dispatching form the core of the solution.
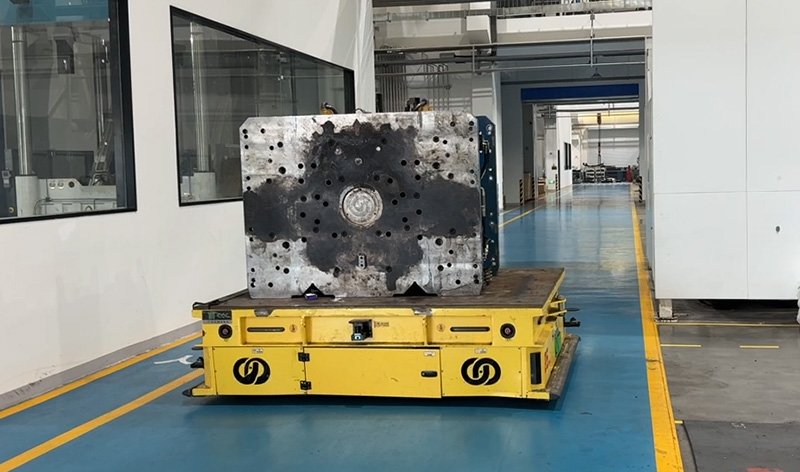
Project at a glance
| Item | Project configuration |
|---|---|
| Industry | Mold manufacturing and assembly |
| Location | Taizhou, Zhejiang, China |
| Application | Transfer between machining, assembly, mold trial and onward handling areas |
| Fleet | Six AGVs, each rated for a 25-metric-ton payload |
| Specified vehicle plan dimensions | 2,300 × 1,900 mm, subject to the approved design drawing |
| Navigation | 3D laser navigation |
| Movement | Longitudinal travel, lateral travel and 360° rotation in place |
| Charging | Six automatic chargers |
| System scope | Fleet dispatching, server, central control console and workshop wireless network |
| Production integration | MES interface specified for app-based vehicle calls linked to process plans |
Configuration figures are drawn from the project technical agreement. They describe the specified system and are not a production performance guarantee.
The challenge: mold transfer across multiple workstations
The factory’s precision machining and assembly workshops are connected by a corridor, with mold trial areas forming another destination in the production flow. After machining, mold components move to assembly and then to trial or inspection. A mold that requires further work returns to the relevant process instead of continuing directly to onward handling.
This creates a transport network with changing origins and destinations. Vehicle availability, loading time and access to shared routes all affect how effectively the line can move work between processes.
The project therefore required more than a heavy-load platform. HENSEN needed to coordinate station-to-station transport around the customer’s production sequence and the physical layout of the workshops.
Overhead cranes remain part of loading and unloading. The AGVs provide horizontal transfer between stations; the automation scope concerns material movement and dispatching rather than every mold assembly operation.
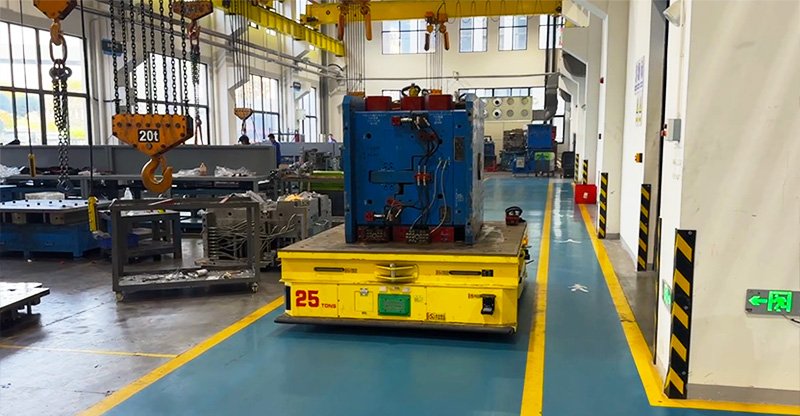
A compact 25-ton AGV for mold handling
Heavy molds concentrate considerable weight within a relatively small footprint. HENSEN specified a 25-ton AGV with a plan size of 2.3 × 1.9 meters to accommodate the load while limiting the space occupied by the vehicle in workshop aisles.
The vehicle uses differential steering drive units for longitudinal and lateral movement, as well as rotation in place. These movements support alignment with workstations and changes of direction within the planned transport network.
Compact dimensions do not remove the need for clearance planning. The technical agreement defines route and turning-space requirements, making aisle geometry, load overhang and station access part of the installation design.
Two 3D laser navigation sensors are specified for each AGV. The agreement lists a travel speed range of 0–30 m/min and straight-line travel accuracy of ±15 mm. The accuracy figure refers to straight-line travel; it should not be interpreted as a verified docking tolerance at every workstation.
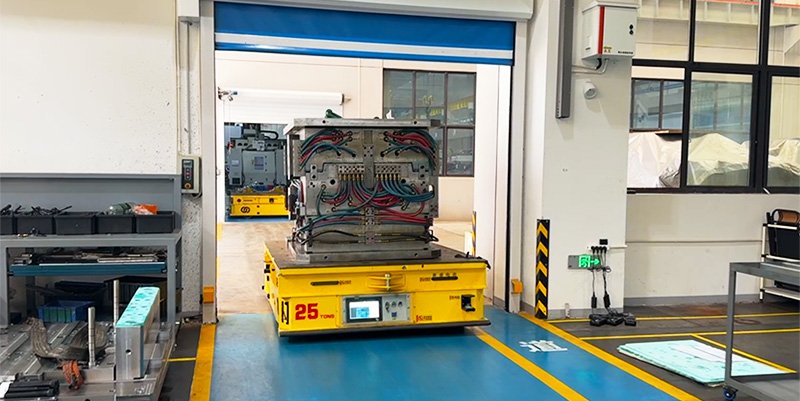
Connecting AGV dispatching with MES process plans
A central feature of the project is the specified interface between the AGV dispatching system and the customer’s manufacturing execution system (MES).
The intended workflow lets an operator select a process in the customer app and call an AGV, with the transport task linked to the associated process plan. This connects the material movement request with its production context: which process needs the mold, where it should go, and what transport task should be issued.
The dispatching specification covers vehicle assignment, route selection, and coordination on shared paths. It includes directing an opposing vehicle to an available side station when needed, coordinating following vehicles, and stopping with a warning when an obstacle is detected. Excessive waiting can trigger an alert for operator intervention.
This approach supports a flexible assembly workflow in which a mold can proceed to trial or return for further work, according to the next required process.
Using simulation to evaluate fleet operation
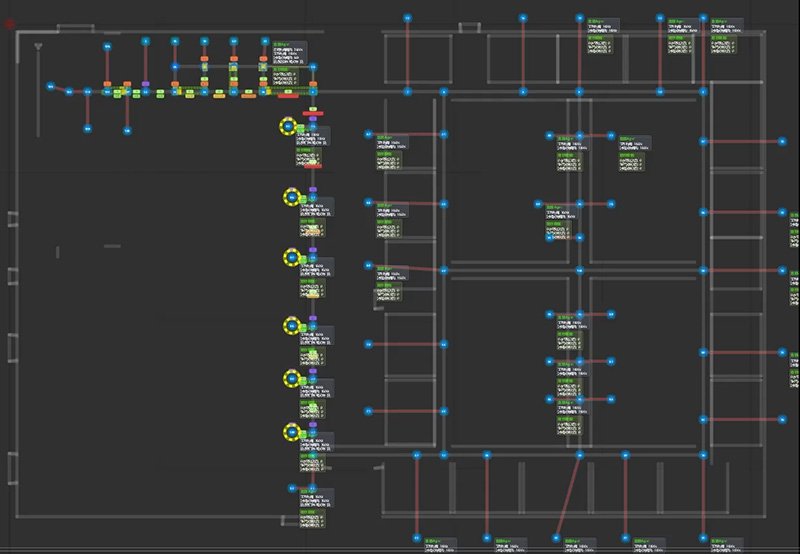
HENSEN carried out transport simulations during planning to examine how vehicles could serve the workshop layout and process flow. The supplied simulation material explores vehicle operation under stated assumptions about travel speed, turning time, loading and unloading, and process duration.
For this project, simulation helped make the proposed transport logic easier to assess before implementation. It also highlighted why loading time and process occupancy matter: an AGV waiting for a mold or a station is unavailable for another transfer.
Simulation results are planning evidence, not measured factory throughput. The source presentation explicitly notes that actual production is affected by people, operating conditions, and process timing. For that reason, no simulated transport count is presented here as an achieved production result.
Automatic charging and practical site preparation
The system includes six automatic chargers. The specified control logic sends vehicles to charge during idle periods or when battery charge falls below the configured threshold; the agreement specifies 20% for low-charge return.
Site discussions highlighted three practical requirements for the charging area: a level docking surface, protection from water accumulation, and sufficient space for the vehicle to align with the charger. Power provision and charger positioning also need to be coordinated with the workshop layout.
These details affect the reliability of automatic charging and the availability of the fleet. Charging strategy must be considered together with transport demand and production schedules.
Safety provisions for shared factory routes
The specified equipment includes emergency-stop switches at the four vehicle corners, audible and visual warnings, and front and rear rubber safety edges. Obstacle-stop behavior and traffic coordination are also included in the dispatching requirements.
The application depends on clear travel paths, suitable floor conditions and defined workstation handling procedures. Vehicle safety features, workshop layout and operating practices need to work together, particularly where AGV routes meet crane loading areas or pedestrian traffic.
What this project demonstrates
The case illustrates how heavy-duty AGVs can be engineered around a mold manufacturer’s actual process flow. The project combines a compact high-load vehicle, flexible movement, coordinated dispatching, and an interface to production planning within one transport system.
Its practical value lies in organizing the connections between machining, assembly and trial operations. The available records do not establish a measured throughput increase, labor saving or final system acceptance date, so those outcomes are not claimed.
For a similar mold assembly project, the starting points are the maximum load and dimensions, workstation sequence, rework routes, loading method, shared aisle conditions and MES task requirements. Together, these determine how the AGV fleet should support the line.
Frequently asked questions
How many AGVs are specified for this mold assembly project?
The project specifies six HENSEN AGVs, each with a rated payload of 25 metric tons, plus six automatic chargers and a centralized dispatching system.
Do the AGVs assemble the molds automatically?
Their role is automated mold transfer between production stations. Overhead cranes remain part of loading and unloading, and the case does not describe fully automated mold assembly.
How are transport tasks linked to production plans?
The project specifies an interface to the customer’s MES. The intended workflow allows an operator to select a process in an app and call an AGV, with the transport request linked to the process plan.
Can the vehicles move sideways in the workshop?
Yes. The specified drive arrangement supports lateral and longitudinal movement and 360° rotation in place, with the required clearances determined by the vehicle, load, and route layout.
Does the simulation prove the fleet’s production capacity?
No. It evaluates operation under defined assumptions. Actual capacity depends on loading, unloading, process duration, traffic conditions and vehicle availability.
For a custom mold transfer system, share your load, workstation layout, and process flow with HENSEN to evaluate the appropriate AGV configuration.