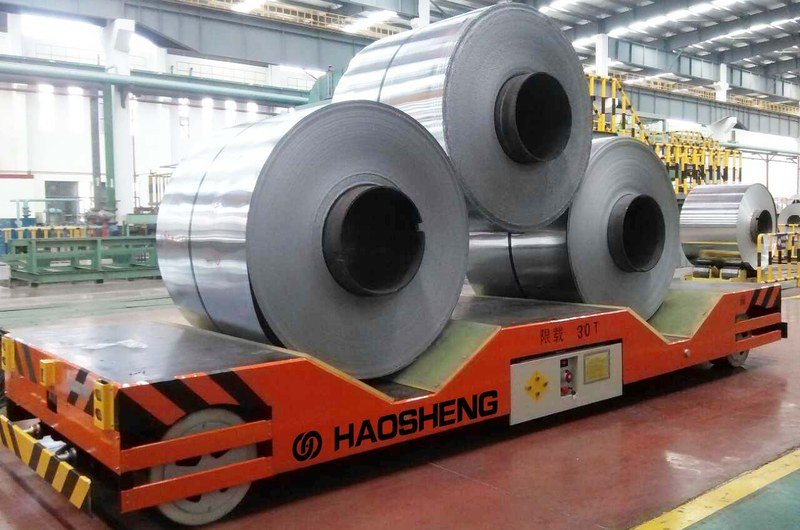
A steel coil is a wheel waiting for permission to roll. Set one on a flat deck and everything depends on chocks, straps and hope; the coil’s own geometry works against you for the entire journey. A steel coil transfer cart solves the problem at the source: a V-shaped deck cradles the coil so that gravity — the force trying to roll it — becomes the force holding it still.
That single geometric idea carries a lot of engineering on its back. The V angle sets contact stresses on the coil’s outer wraps; the saddle lining decides whether prime surface arrives unmarked; the structure beneath must take a concentrated line load rather than a spread one; and the cart’s stopping accuracy determines whether a coil car can shake hands with cranes, down-enders, turnstiles and automated coil yards.
This guide covers each layer in turn: V-deck geometry, anti-roll security beyond geometry, capacity and structural design across the 10–200 ton range, and the automation ladder from a pendant-controlled cart to a coil car that answers directly to the WMS.
Why Coils Need a Dedicated Transfer Cart
Coils concentrate enormous mass into a shape that is both mobile and fragile. The mass wants to roll along the deck; the surface — especially on cold-rolled, coated or prime material — bruises against any hard edge; and the wound structure can telescope or collapse if supported carelessly. Flat-deck carts, forklifts with coil rams and improvised cradles each compromise on at least one of these fronts.
A purpose-built coil car addresses all three at once: the V-deck locks the cylinder against rolling, engineered saddle liners protect the wraps, and support along two lines of contact — rather than a point or a single line — respects the coil’s structure. On a fixed route between a slitter, storage bays and a loading area, a rail-mounted coil cart adds determinism: same path, same stop, every cycle. For the broader family this vehicle belongs to, see our complete RGV guide; here we stay with coils.
V-Deck Geometry: How the Angle Does the Work
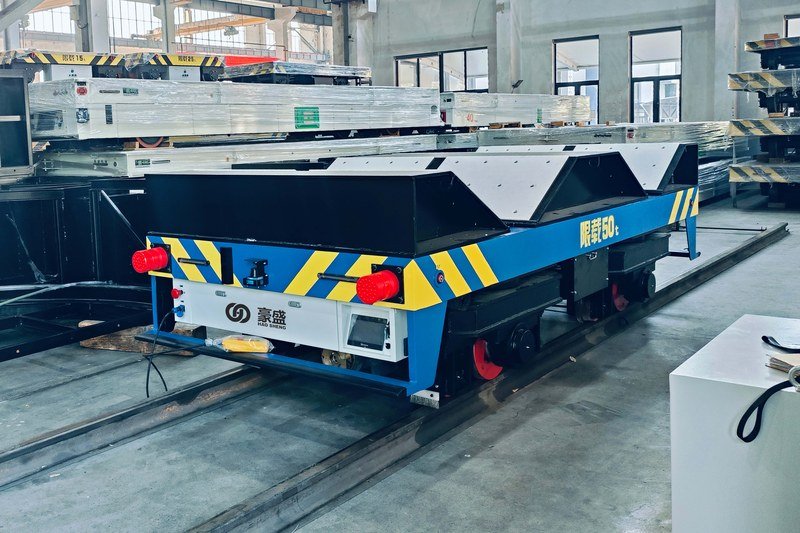
The included angle and contact lines
A coil in a V-deck rests on two contact lines, one on each face of the V. The included angle controls the trade-off. A shallow, wide V lowers the coil’s center of gravity less and produces higher force pressing the coil into each face — good grip, higher contact stress on the outer wrap. A steep, narrow V cradles deeply but concentrates load near the coil’s underside and limits the diameter range that seats properly. Practical coil cars settle in the middle, sized so that the smallest and largest coils in the mix both make clean two-line contact without touching the V’s root or riding its edges.
Sizing for your coil mix
The V must be specified against the real coil population: minimum and maximum outside diameter, width range, and worst-case weight. A V cut for 1,800 mm coils will let a small-diameter coil sit low and nearly wedge; a V cut for small coils leaves a large one perched high with reduced grip. Where one cart must serve a wide diameter spread, the answer is usually a longer V with carefully chosen face angles, or interchangeable saddle inserts rather than one compromised profile.
Saddle liners and surface protection
Bare steel Vs are for hot-rolled black coil only. For anything surface-critical, the faces carry replaceable liners — polyurethane pads, hardwood, or engineered polymer strips — that spread contact pressure and prevent wrap marking. Liners are bolted consumables: they wear, they are inspected, they are swapped in minutes. Specify the liner material against coil temperature as well as surface class, since coil fresh off some lines arrives too hot for standard polyurethane.
Anti-Roll Security Beyond Geometry
The V does most of the work, but a moving cart adds dynamics that geometry alone should not be asked to absorb. Coil cars in this class layer three further protections.
- Soft motion control — variable-frequency drives deliver stepless 0–20 m/min travel with programmed soft start and soft stop, so the coil never receives a jolt that could shift it in the V or telescope its wraps.
- Fail-safe braking — spring-applied electromagnetic brakes clamp automatically on any power loss, and mechanical end stops with buffers guard the rail ends.
- Load sensing and interlocks — coil-presence sensors confirm seating before travel is enabled, and travel is inhibited during crane or magnet handover so cart and crane never fight over a suspended coil.
The standard safety set completes the picture: 270° laser obstacle scanning front and rear, four-corner emergency stops, and audible-visual alarms. None of it is coil-specific, all of it matters more when the payload is a 40-ton cylinder.
Capacities and Structural Design
Coil transfer carts commonly span 10 to 200 tons — from single slit coils feeding a stamping shop to master coils and multi-coil decks in a hot-strip mill — within a rail-cart platform family that runs from 1 to 500 tons. The V-deck changes how the structure is loaded: instead of a distributed deck load, the frame receives two concentrated line loads at the V faces, so the box-beam layout underneath is arranged to carry them directly into the wheel groups.
Construction follows heavy-RGV practice: Q345 box-beam frames welded and then stress-relieved by post-weld annealing, machined in a single gantry setup so V faces and wheel seats stay true, with deflection under rated load held to roughly L/1000 of the wheelbase. Rails are crane-type P38, P43 or P50 depending on wheel loads, installed to about ±2 mm level and ±5 mm gauge. Every cart is load-tested at 1.1× rated capacity before shipment.
| Capacity class | Typical duty | 2026 ex-works budget (RGV) |
| 10–50 t | Slit coils, line feeding, press shops | $25,000–80,000 |
| 50–150 t | Master coils, slitter-to-storage, bay transfer | $60,000–180,000 |
| 150–200 t | Heavy mill coils, multi-coil decks | from $150,000 (150–500 t band: $150,000–500,000+) |
Options that move a cart within its band include hydraulic lifting V-decks (150–400 mm stroke, multi-cylinder synchronization within ±1 mm) for picking coils off storage saddles, weighing systems, and rotating decks for orientation changes. The full cost logic lives in our RGV price guide.
Power Options for Coil Routes
Three supply systems cover coil-cart duty. LiFePO4 lithium battery power with automatic opportunity charging suits flexible routes and 24/7 multi-shift mills. AC36V low-voltage rail power — 380V stepped down through transformer cabinets roughly every 50 m with copper-bar compensation — suits fixed high-frequency shuttles where charging downtime is unacceptable. Drag cable remains the economical answer for short straight runs up to about 50–80 m, such as a slitter-to-bay shuttle.
Automation: From Pendant Control to Coil Yard Integration
Coil cars ship in automatic, semi-automatic and manual modes, and plants typically climb the ladder in stages.
Manual and semi-automatic operation
An operator drives from a pendant or the onboard 7-inch touchscreen; in semi-automatic mode the cart executes pre-programmed station-to-station moves on command. Manual top speed is capped around 25 m/min.
Automatic station-to-station cycles
RFID station identification plus laser ranging give ±5 mm stopping accuracy — precise enough for repeatable handovers to down-enders, turnstiles, walking beams and coil ramps without an operator lining anything up.
Full coil yard integration
The cart’s PLC connects to the mill’s WMS or MES over industrial WiFi or 5G using TCP or MQTT. The warehouse system assigns each coil a saddle position, dispatches the cart, tracks the move, and updates inventory on completion — the coil car becomes one node in an automated coil yard alongside cranes and storage saddles.
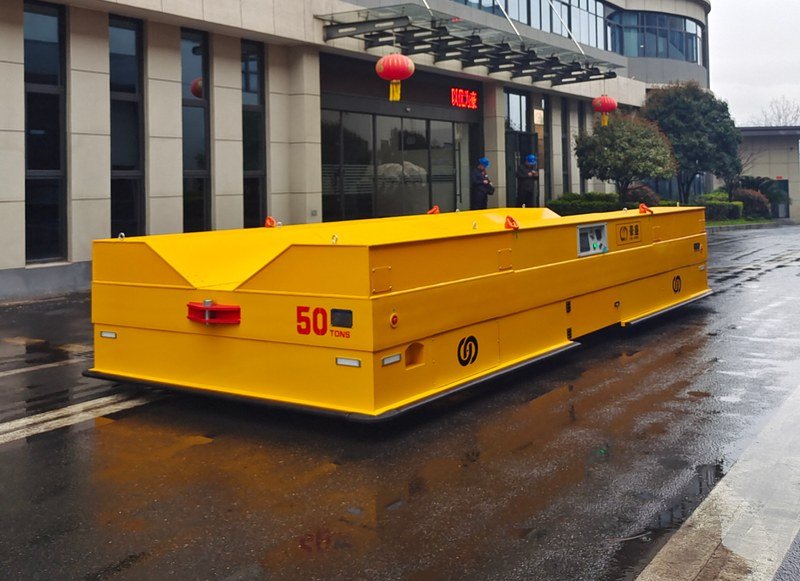
For plants going trackless, the same V-deck rides on heavy AGVs: HENSEN’s references include a 50-ton V-deck AGV whose 3D SLAM navigation (about ±10–15 mm, no reflectors) and omnidirectional steering suit yards where routes change with the storage plan. Rails remain the cheaper, more repeatable choice on fixed routes.
Feeding Processing Lines and Other V-Deck Duties
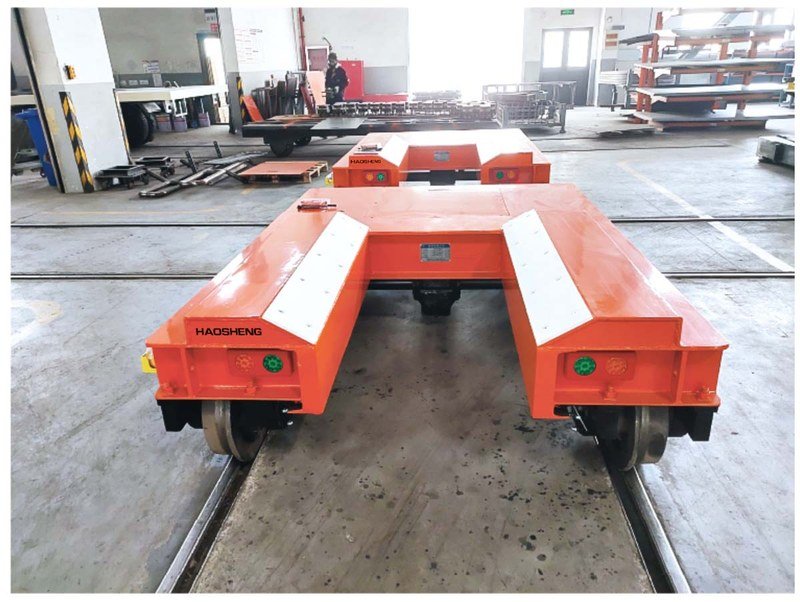
A large share of coil cars spend their lives as line feeders: shuttling coil from storage saddles to the entry of a slitting, cut-to-length or coil-leveling line on a fixed cycle. HENSEN’s delivered examples include an RGV feeding coil stock to a leveling line, where the lifting V-deck picks the coil off saddles and presents it at the uncoiler’s mandrel height. The same V-deck principle serves any cylinder that must not roll — cable reels, pipe, and drums — a topic we cover separately in our cable reel and coil handling V-deck RGV guide.
Delivery for a custom coil car typically runs 3–4 months from signed technical agreement to factory acceptance, service life is 10–15 years or more, and multi-shift operations commonly recover the investment in about 2–4 years.
HENSEN (Hangzhou Haosheng Electric Vehicle Co., Ltd.) designs and builds V-deck coil transfer carts and coil-handling RGVs from 1 to 500 tons — plus heavy-duty AGVs up to 800 tons — with in-house control and scheduling software, CE marking and ISO 9001 certified manufacturing, delivered across wind power, metallurgy, sheet metal, and construction machinery plants worldwide. Send us your coil diameter range, weights, and route sketch, and our engineers will propose a V-deck configuration with budget pricing.
FAQ About Steel Coil Transfer Carts
Q: What V angle should a coil transfer cart have?
A: There is no universal angle — the V is sized against your coil mix. The faces must give clean two-line contact across your minimum and maximum coil diameters, without small coils wedging near the root or large coils perching on the edges. State your OD range, width range, and worst-case weight, and let the manufacturer cut the V to fit.
Q: How is a coil kept from rolling during transport?
A: Primarily by the V geometry itself, which turns gravity into the holding force. On top of that, soft start/stop motion control (0–20 m/min, stepless) prevents jolts, coil-presence sensors interlock travel until the coil is seated, and spring-applied electromagnetic brakes clamp automatically if power is lost.
Q: Will a V-deck mark prime or coated coil surfaces?
A: Not if the faces are lined. Replaceable polyurethane, hardwood or polymer liners spread the contact pressure over the outer wrap and are swapped as consumables. Specify liner material against both surface class and coil temperature — hot coil needs heat-tolerant liners.
Q: What capacities do steel coil transfer carts come in?
A: Common builds run 10 to 200 tons — slit coils at the light end, master mill coils at the heavy end — within a platform family spanning 1 to 500 tons. Every HENSEN cart is factory load-tested at 1.1× rated capacity before shipment.
Q: Can a coil cart work inside an automated coil yard?
A: Yes. With RFID-plus-laser positioning (±5 mm) and a PLC linked to the WMS or MES over WiFi or 5G via TCP or MQTT, the cart takes move orders directly from the warehouse system and reports completion — no operator in the loop. This is the standard architecture for automated coil storage.
Conclusion
A steel coil transfer cart succeeds by respecting one shape. The V-deck turns the coil’s urge to roll into stability; liners and two-line support protect the wraps; an annealed box-beam frame carries the concentrated loads; and soft motion, interlocks and fail-safe brakes handle the dynamics geometry cannot. From a 10-ton line feeder to a 200-ton mill car — manually driven or answering to the WMS — the specification starts in the same place: your real coil mix, honestly stated. Get the V right, and everything above it follows.
Leave a comment